Achieving quality MIG welds relies fundamentally on precise control over shielding gas pressure and flow. Incorrect gas settings lead to common welding defects like porosity, excessive spatter, and poor penetration, costing time and materials in rework. Understanding the distinction between cylinder pressure, regulator function, and flow rate is critical for any welder aiming for consistent, strong welds across various materials and applications.
Understanding MIG Shielding Gas and Its Purpose
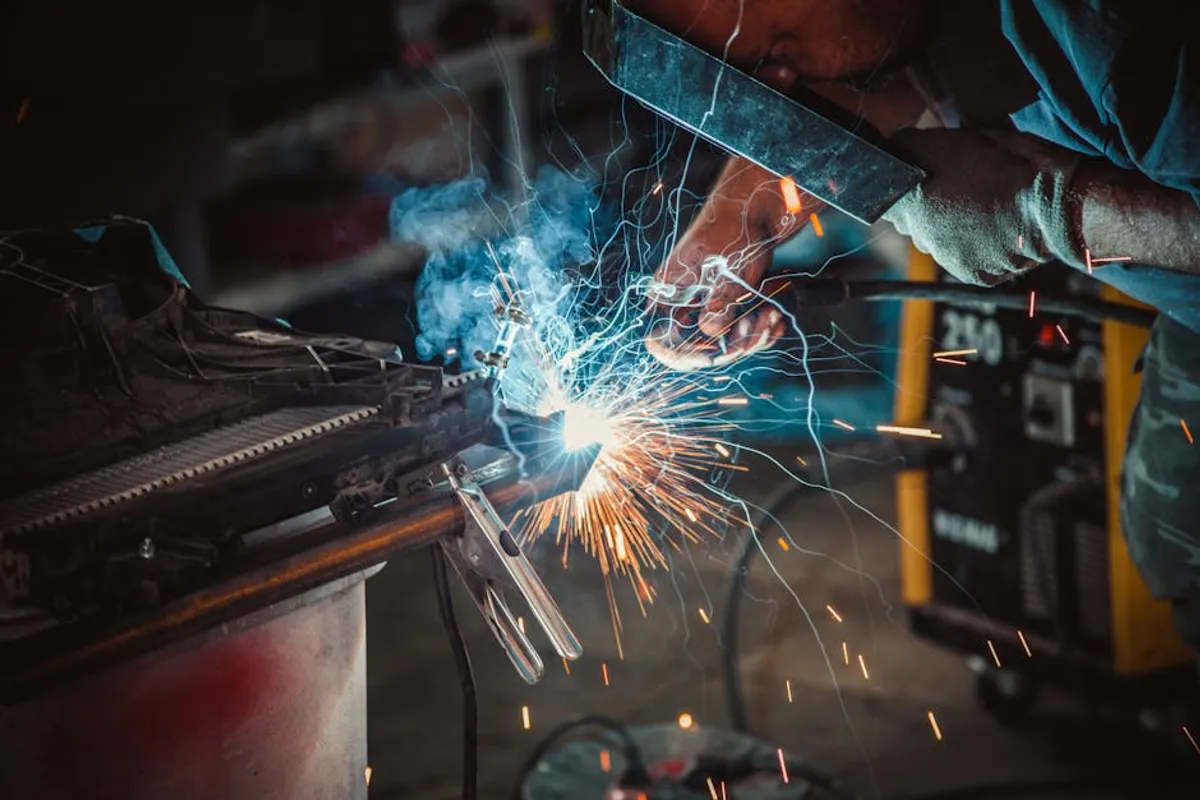
MIG welding (Gas Metal Arc Welding, GMAW) uses a continuous wire electrode fed through a welding gun, creating an arc between the wire and the workpiece. Shielding gas delivered through the gun nozzle protects the molten weld pool from atmospheric contamination, specifically oxygen and nitrogen. Without proper shielding, the weld becomes brittle, porous, and prone to cracking. The effectiveness of this shield is directly tied to the gas type and its flow rate.
Common shielding gases include:
- Argon (Ar): An inert gas, suitable for aluminum, stainless steel, and other non-ferrous metals. It produces a stable arc and minimal spatter.
- Carbon Dioxide (CO2): An active gas, more economical and provides good penetration for steel. However, it can produce a harsher arc and more spatter than argon blends.
- Argon/CO2 Blends: The most common choice for mild steel, offering a balance of arc stability, penetration, and reduced spatter. Typical blends are 75% Argon/25% CO2 (75/25) or 90% Argon/10% CO2 (90/10).
- Argon/Oxygen Blends: Used for spray transfer on stainless steel and some carbon steels, improving arc stability and wetting action.
Each gas or blend has specific properties that influence arc characteristics, heat input, and weld bead appearance, making gas selection a crucial first step before setting pressure.
Regulators and Flowmeters: Controlling Gas Delivery
While a gas cylinder holds shielding gas at pressures typically ranging from 2000 to 2200 PSI, this pressure is far too high for direct welding use. A regulator is essential to reduce this high cylinder pressure to a safe, usable working pressure. However, for MIG welding, the critical measurement is not pressure in PSI at the torch, but the flow rate of gas in cubic feet per hour (CFH) or liters per minute (LPM).
This is where the flowmeter comes in. Often integrated into the regulator unit, the flowmeter measures the actual volume of gas flowing to the welding gun. It typically features a ball floating in a tapered tube, indicating the CFH. Setting the correct CFH is paramount, as it directly controls the effectiveness of the gas shield around the weld pool.
Pro Tip: Always check for gas leaks before starting any welding project. Apply a soapy water solution to all connections (cylinder valve, regulator, hose fittings). Bubbles indicate a leak, which wastes gas and compromises weld quality. Address leaks immediately by tightening connections or replacing faulty seals.
Setting Optimal Flow Rates for Various Applications
The ideal gas flow rate varies based on several factors, including the type of material, joint configuration, welding position, and environmental conditions. General guidelines exist, but fine-tuning is often necessary:
- Mild Steel (Short-Circuit Transfer): For 75/25 Argon/CO2, common flow rates range from 15-25 CFH (7-12 LPM). Thicker materials or higher amperage may require slightly more.
- Aluminum: Using 100% Argon, flow rates typically fall between 20-30 CFH (9-14 LPM). Aluminum's higher thermal conductivity and the need for a robust shield often necessitate a slightly higher flow.
- Stainless Steel: With Argon/CO2 or Argon/Oxygen blends, 18-28 CFH (8-13 LPM) is a common range.
- Windy Conditions: In outdoor or drafty environments, flow rates may need to be increased by 5-10 CFH to compensate for shield disruption. However, excessive flow can lead to turbulence and draw contaminants into the weld.
An insufficient flow rate fails to protect the weld pool adequately, leading to porosity. Conversely, an excessive flow rate can create turbulence, pulling atmospheric air into the shield, also causing porosity, or simply wasting gas without benefit.
Impact of Gas Pressure on Weld Quality
The primary impact of gas pressure (as translated to flow rate) on weld quality is directly related to shielding effectiveness. A consistent and adequate flow rate ensures the molten metal is fully enveloped by the inert or active gas, preventing oxidation and nitridation.
Specific quality considerations:
- Porosity: The most common defect from inadequate shielding. Gas bubbles become trapped in the solidifying weld metal, creating small holes. This significantly weakens the weld.
- Spatter: While wire feed speed and voltage are primary factors, incorrect gas flow can exacerbate spatter. Too low flow can lead to an unstable arc, increasing spatter.
- Arc Stability: Proper gas flow contributes to a smooth, stable arc. Erratic flow can cause the arc to wander or extinguish, leading to inconsistent penetration and bead appearance.
- Penetration and Bead Profile: While gas type (e.g., CO2 for deeper penetration) plays a larger role, consistent shielding allows the arc to focus its energy efficiently, contributing to a well-formed, uniform bead with appropriate penetration.
- Weld Strength and Ductility: Contaminated welds (due to poor shielding) are inherently weaker and less ductile, making them prone to failure under stress.
Buying Tips for Regulators and Flowmeters
Selecting the right regulator and flowmeter is an investment in consistent weld quality and gas efficiency. Consider these factors:
Type of Regulator:
- Single-Stage Regulators: Reduce cylinder pressure in one step. They are generally more affordable but may show a slight pressure drop as the cylinder empties, requiring minor adjustments. Suitable for hobbyists or intermittent use.
- Dual-Stage Regulators: Reduce pressure in two steps, providing a more constant output pressure regardless of decreasing cylinder pressure. This offers superior stability and consistency, ideal for professional use or critical applications where precise flow is paramount.
Flowmeter Design:
- Ball-Type Flowmeters: The most common, using a floating ball in a vertical tube to indicate CFH. Ensure the scale is easy to read.
- Bourdon Tube Flowmeters: Less common for MIG, but offer a dial gauge reading.
Gauge Quality and Readability: Look for clear, large gauges that are easy to read. Gauges should be robust and protected from accidental impact. Dual gauges (one for cylinder pressure, one for regulated pressure/flow) are standard and necessary.
Material and Construction: Regulators are typically brass or chrome-plated brass for durability and corrosion resistance. Ensure robust construction to withstand workshop environments.
Inlet and Outlet Connections: Verify that the regulator's inlet connection matches your gas cylinder (e.g., CGA 580 for inert gases like Argon/Argon blends). The outlet connection should match your welding hose.
Serviceability and Parts Availability: Consider brands that offer replacement parts (e.g., diaphragms, gauges) and readily available service.
Maintaining Your Gas Delivery System
Regular maintenance ensures optimal performance and safety. Check all hoses for cracks or damage periodically. Inspect O-rings and seals on fittings and the regulator for wear. Always store cylinders upright and secured. When changing cylinders, ensure the valve threads are clean and free of debris before attaching the regulator. Never use oil or grease on oxygen or acetylene cylinder connections, but for MIG shielding gases, ensure clean, dry connections.
Frequently Asked Questions
What is the ideal gas flow rate for MIG welding mild steel with 75/25 Argon/CO2?
A common starting point is 15-25 CFH (cubic feet per hour), or 7-12 LPM (liters per minute). Adjust within this range based on material thickness, joint type, and any environmental drafts.
Why am I getting porosity in my MIG welds even with gas flowing?
Porosity can stem from several issues: gas flow too low or too high (causing turbulence), gas leaks in the system, contaminated base metal, dirty wire, or a clogged gun nozzle. Check all connections, clean the workpiece, and ensure your flow rate is within the recommended range.
Does cylinder pressure affect my weld quality?
Directly, no. Your regulator reduces the high cylinder pressure to a usable level, and your flowmeter then controls the actual gas flow rate (CFH) to the torch. However, if cylinder pressure drops too low, a single-stage regulator may struggle to maintain consistent output, potentially affecting flow. A dual-stage regulator mitigates this.
How do I know if my regulator or flowmeter is faulty?
Signs of a faulty unit include inconsistent gas flow despite stable cylinder pressure, visible leaks around the unit, gauges that don't register correctly, or a ball in the flowmeter tube that sticks or vibrates erratically. If you suspect a fault, have it inspected by a qualified technician.